About Protease Enzyme Powder
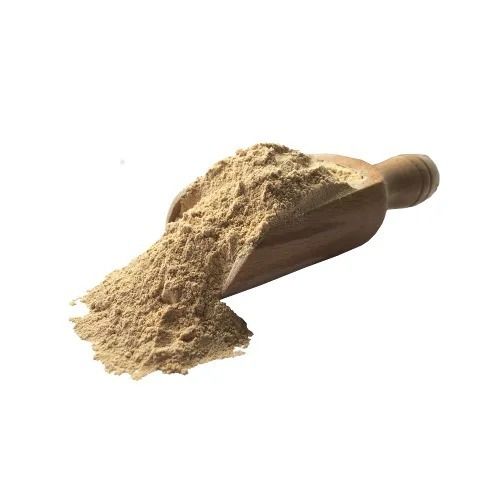
Proteases regulate the fate, localization, and activity of many proteins, modulate protein-protein interactions, create new bioactive molecules, contribute to the processing of cellular information, and generate, transduce, and amplify molecular signals.Exceptional Performance Across IndustriesProtease Enzyme Powder delivers reliable proteolytic activity for diverse industries, including food processing, pharmaceuticals, detergents, and leather treatment. Its high activity and broad optimum temperature and pH ranges make it adaptable to various production environments. With consistent efficacy, it is trusted by manufacturers, exporters, and suppliers across India.
Safety and Quality AssuranceThis enzyme powder is manufactured to high standards, ensuring it is pathogen-free and contains no common allergens. Each batch is free from heavy metals and complies with industrial and food-grade purity criteria. Proper use of personal protective equipment is advised to prevent inhalation or contact, maintaining both user safety and product integrity.
Easy Handling and Long Shelf LifePackaged securely in 25 kg drums or boxes, Protease Enzyme Powder remains stable for up to 24 months when stored in a cool, dry place below 25C. Its fine, water-soluble form allows for easy integration into production processes, supporting operational efficiency and sustained quality over time.
FAQ's of Protease Enzyme Powder:
Q: How should Protease Enzyme Powder be used in industrial or food applications?
A: Protease Enzyme Powder can be added directly to processes like baking, brewing, protein hydrolysis, detergents, and leather treatment, with dosing based on specific application requirements. Ensure the enzyme is used within the recommended temperature (40C-60C) and pH (7.0-8.0) ranges for optimal activity.
Q: What are the main benefits of using this enzyme powder?
A: This enzyme powder efficiently breaks down proteins, improving product texture, processing speed, and overall output quality. Its non-toxic and pathogen-free composition makes it safe for use in both industrial and food-grade applications.
Q: When is it best to incorporate Protease Enzyme Powder into a production process?
A: For best results, introduce the enzyme during stages where protein hydrolysis or modification is needed, such as the mixing phase in baking, or during substrate exposure in brewing and detergents. Always follow your process guidelines for specific timing.
Q: Where is Protease Enzyme Powder typically used?
A: It is widely used in the food industry (baking, brewing), pharmaceutical manufacturing, detergent formulations, leather processing, and biotechnological applications such as bio-remediation.
Q: What precautions should be taken when handling Protease Enzyme Powder?
A: Always use personal protective equipment (PPE), such as masks, gloves, and goggles, to avoid inhalation and skin or eye contact. Handle in a well-ventilated area and avoid creating dust.
Q: How is the safety and quality of Protease Enzyme Powder maintained?
A: The powder is manufactured under strict quality controls to ensure it is free from pathogenic contaminants, heavy metals, and common allergens. Each batch meets industrial and food-grade standards, with specified purity and moisture content.
Q: What is the recommended storage process and shelf life for this product?
A: Store the enzyme powder in tightly sealed containers in a cool, dry place below 25C. Under these conditions, the shelf life is up to 24 months without loss of activity or quality.






 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
